
 Lesson 2.3
 · The Spectrum of Off-Site
3D Volumetric Modular
The far end of the spectrum: whole three-dimensional rooms built and finished in the factory, then stacked and connected on site — the maximum of off-site value and speed, bought with weight, transport limits and decisions locked in early
A finished hotel room leaves the factory as a box — carpeted, plumbed, painted, the bed almost made — and arrives on site ready to stack. That is the summit of off-site construction, and it is the least forgiving place to stand.
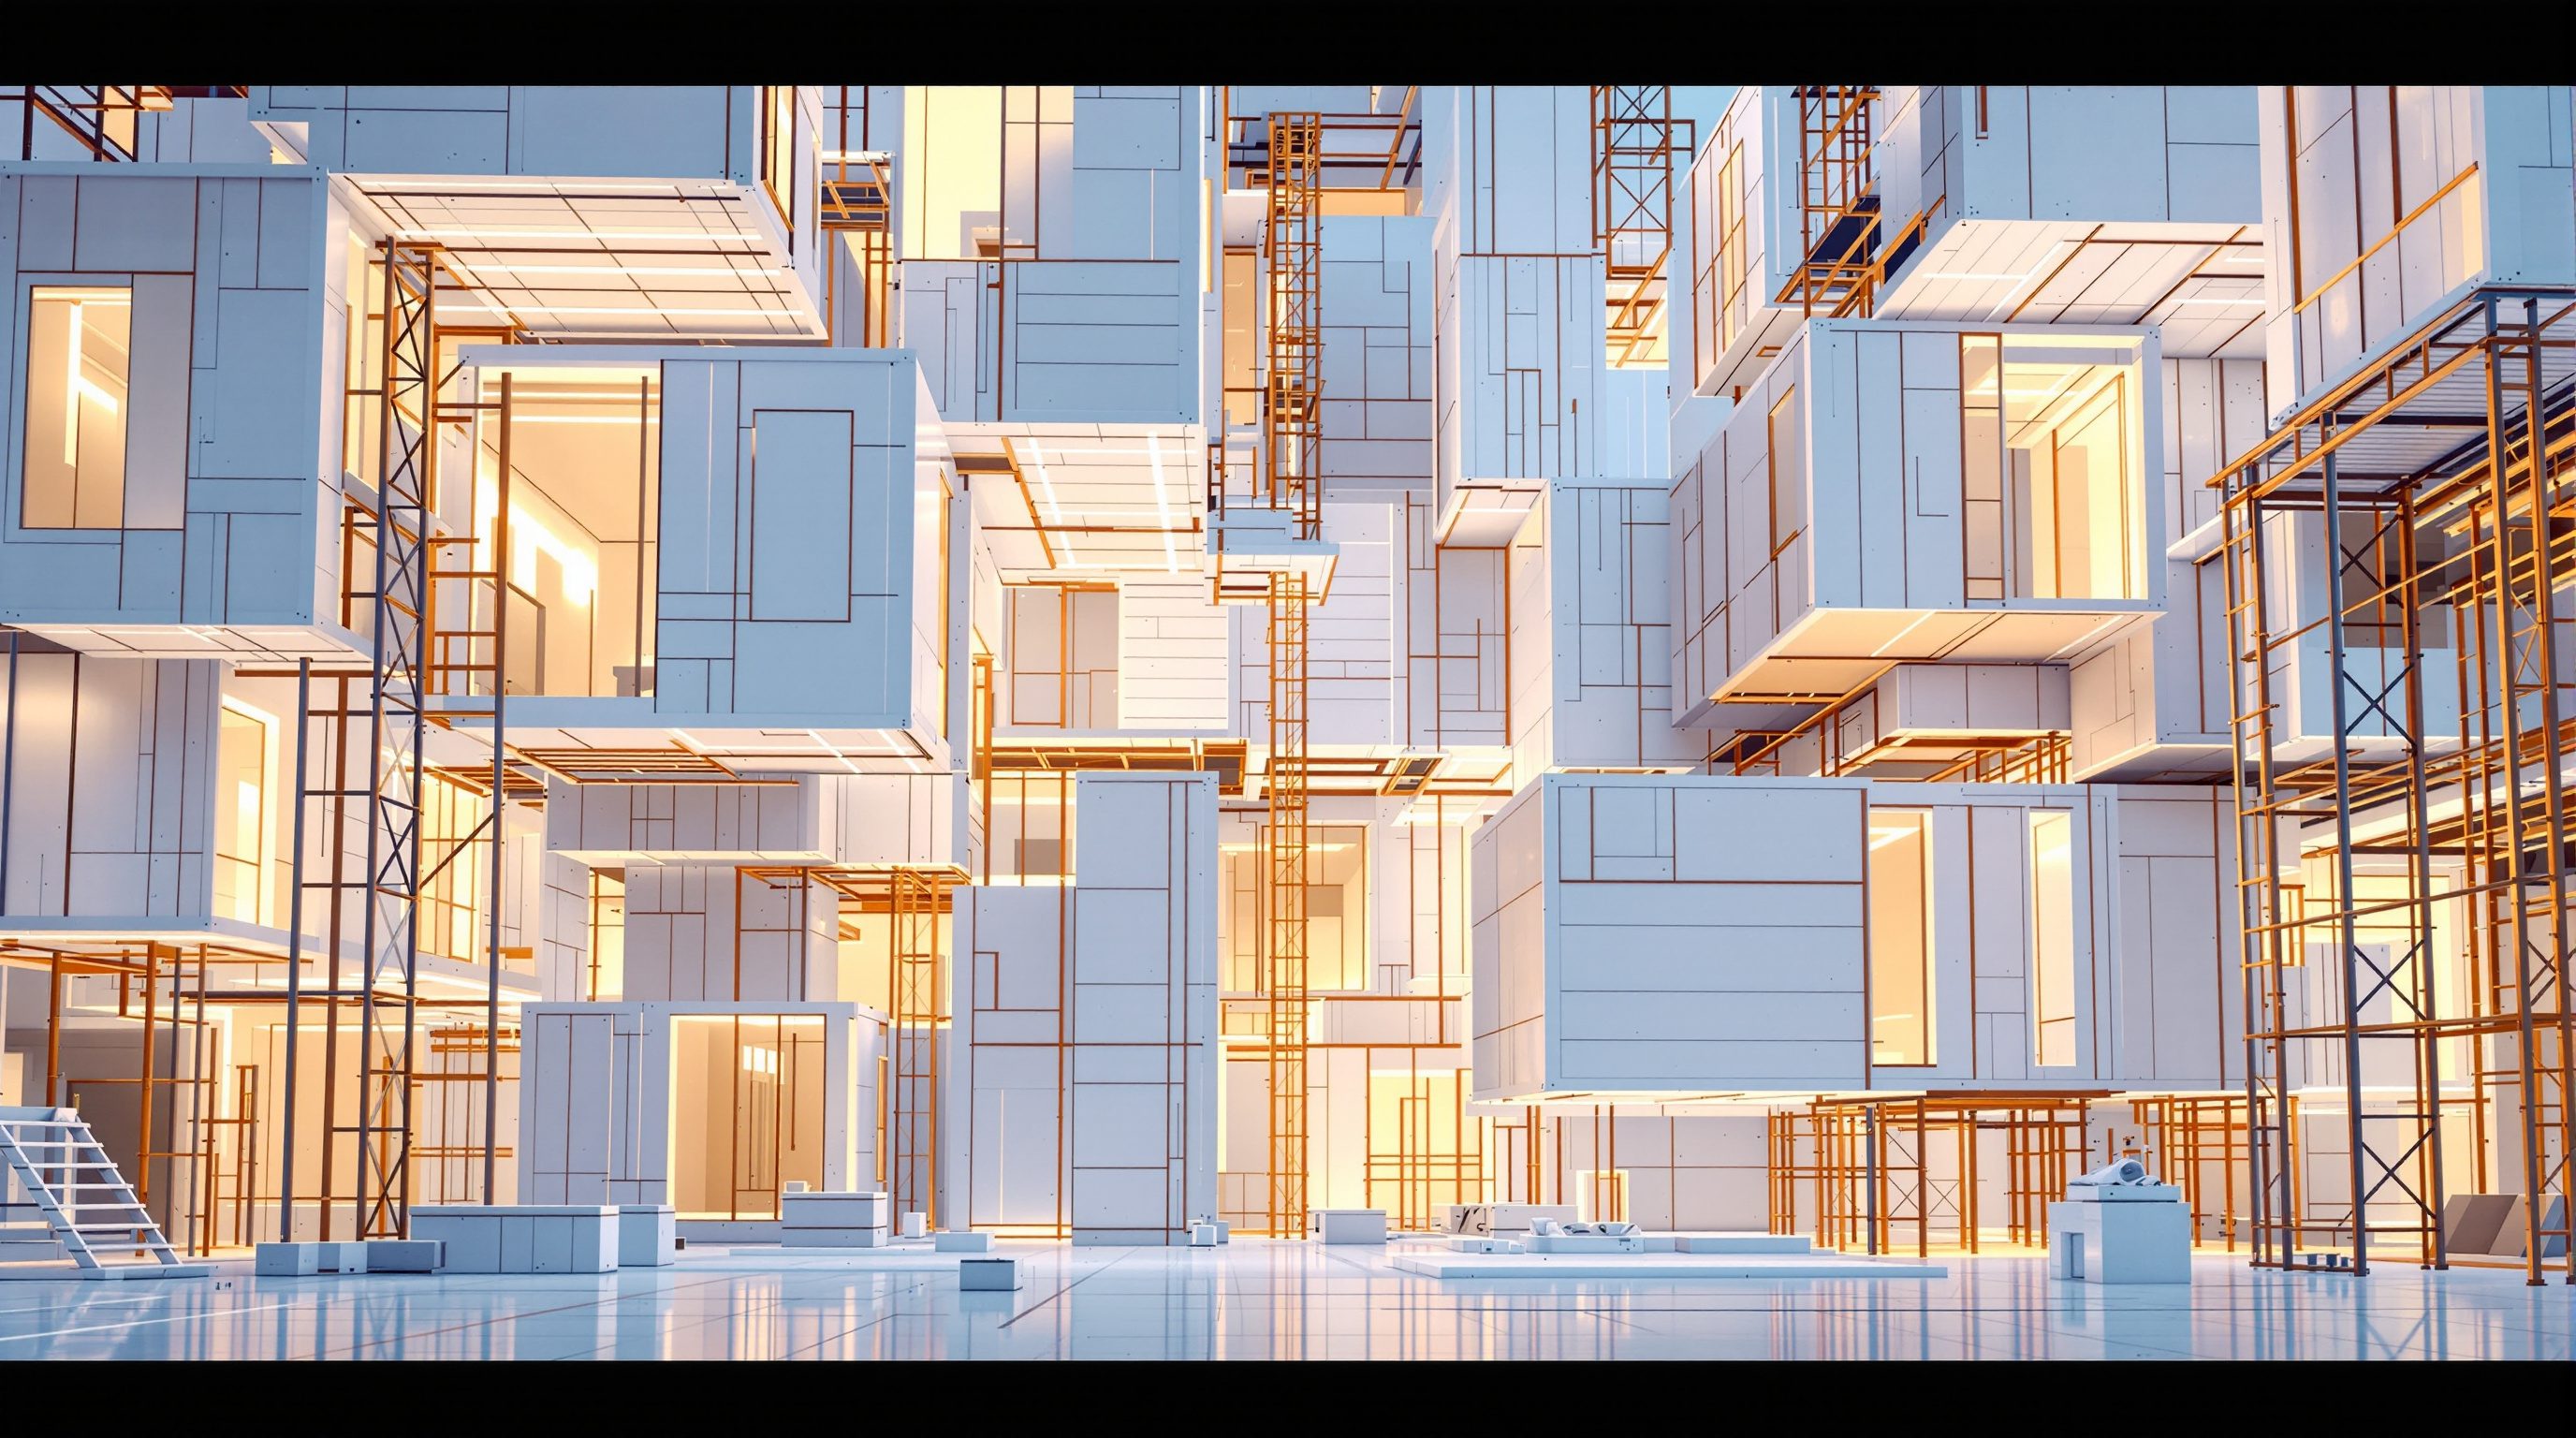
At the far end of the spectrum the factory stops making parts and planes and starts making rooms. In volumetric modular construction, whole three-dimensional chunks of building — a hotel bedroom, a flat, a student room, a hospital ward, a bathroom — are built and finished in the factory as self-contained boxes, complete with structure, walls, ceilings, services, finishes, fittings and sometimes the furniture, then transported to site and stacked and connected into a building. It is the maximum of off-site value: the greatest share of the building made in controlled conditions, the most work removed from the site, and the fastest on-site programme, because the rooms arrive essentially done.
It is also the least forgiving point on the spectrum, and this lesson is as much about the costs as the promise. A finished module is heavy and ships mostly air, so transport is expensive and bounded by a transport envelope — the maximum size the road, the bridges and the permits allow. It is fragile to handle, because a fully finished room does not like being lifted, twisted and craned. Its dimensions are locked in very early, because the factory needs them frozen to build. And where modules meet, you get a double skin — two module walls and two floors back to back — which must be detailed for structure, fire, acoustics and weather. Volumetric is extraordinary where repetition, speed and a suitable site line up; it punishes variety, late change and difficult logistics harder than anywhere else on the spectrum.
Finished rooms, stacked. Max value, max speed — paid for in weight, envelope, fragility, early lock-in, double skin. Load-bearing vs podium. Know when to say no.
What volumetric modular is, and where it shines
A volumetric module is a structural box that is also a finished room. In the factory, a module's floor, walls and ceiling are framed (in light-gauge steel, timber or concrete), then the building-up happens while the box sits at a comfortable working height on a line: insulation, services, plasterboard, flooring, wall and ceiling finishes, doors, windows, bathroom fittings, kitchen units, wardrobes, sometimes even the light fittings, curtains and the made bed. The module is inspected, wrapped and transported to site, where a crane lifts it into position and a crew connects it — structurally, and for services, fire and weather — to the modules and structure around it. A building becomes a stack of finished rooms assembled in days or weeks rather than made in months.
Volumetric shines in a specific and recognisable situation: many near-identical rooms. Hotels are the classic case — a tower of bedrooms that are all the same module, repeated hundreds of times, each benefiting from the factory's learning curve and quality. Student accommodation, key-worker and affordable housing, hospital wards and treatment rooms, prison cells, and above all bathroom and kitchen pods dropped into otherwise conventional buildings are the natural territory. The common thread is repetition: the more times the factory builds the same module, the more the fixed costs of tooling, setup and design are amortised, the further the learning curve runs, and the more the speed and quality advantages land.
The speed is genuinely dramatic, and it comes from two sources. First, the module arrives finished, so the slow, sequential, weather-exposed trades that dominate a site programme — the plastering, the second fix, the tiling, the decorating — already happened in the factory, in parallel. Second, the factory build and the site groundworks happen at the same time: while modules are being manufactured, the foundations, podium and services connections are being built on site, so two long activities that would have been sequential run in parallel. This parallelism, not any single fast operation, is why modular programmes can compress so sharply. But every bit of that advantage is earned by repetition and by getting the design frozen early — which is exactly where the costs of volumetric begin.
A volumetric module is a structural box that is also a finished room. It shines on repetition — hotels, student rooms, wards, pods. Speed comes from parallel factory + site work.
The costs of maximum factory value: weight, envelope, fragility, lock-in, double skin
Volumetric buys the most off-site value, and it pays the most for it. Five costs recur, and a designer must hold all of them from the first sketch.
The first is weight. A finished room — structure, finishes, fittings — is heavy, and weight drives the cost and feasibility of transport and especially craneage: a bigger, heavier module needs a bigger crane, a stronger lifting frame and more substantial connections, and there are limits beyond which a module simply cannot be lifted into position economically.
The second is the transport envelope. A module must travel by road from factory to site, which means it cannot exceed the maximum width, height and length that the roads, bridges, tunnels, roundabouts and permits along the route allow. That envelope — not the designer's preference — sets the maximum module size, and because you are shipping a box of mostly finished air, you are paying to transport volume, not just mass. Long hauls and tight urban sites make volumetric expensive or impossible.
The third is handling fragility. A fully finished room does not enjoy being lifted, craned, twisted and set down; finishes crack, fittings loosen, airtightness layers tear. Modules must be engineered and braced to survive transport and lifting loads that the finished building will never see again, and they must be protected and inspected — a real design and logistics discipline, not an afterthought.
The fourth, and in design terms the deepest, is dimensions locked in early. The factory cannot start until the module design is frozen, and once production runs, changing anything is slow and costly. So volumetric forces the design decisions — room sizes, layouts, services, finishes — to be made and fixed far earlier than any site-built project would demand. This is the single most important thing to understand about designing for volumetric: it is unforgiving of late change, and it rewards certainty.
The fifth is the double skin. Where two modules sit side by side or stacked, you get two walls or two floors back to back, with a gap between — more material, more weight, more thickness, and a junction that must be deliberately designed for structure, fire compartmentation, acoustic separation and weather. The double skin is often an acoustic and fire advantage (two separated layers perform well) but a cost in material, thickness and detailing complexity. None of these five costs is a reason to avoid volumetric; they are the shape of the tool, and designing volumetric well means designing with all five in mind and deferring their binding engineering to the specialists.
Two ways modules carry load: load-bearing and frame-supported (podium)
How a modular building stands up is a fundamental design decision, and it splits into two broad structural strategies that shape everything above them. Understanding the difference is core to reading and designing a volumetric building.
In load-bearing (corner-supported) modular, the modules themselves carry the building's loads: each module is a structural box that sits directly on the one below and transfers weight down through its corners and walls to the foundation. The whole building is, in effect, a neat stack of structural boxes. This is efficient and simple for regular, repetitive buildings where modules sit tidily on top of one another — classic hotel and student-housing towers — but it limits how high you can go (the lowest modules must carry everything above, and module structure has practical limits), and it rewards a disciplined, regular stack where loads run cleanly down through aligned modules.
In frame-supported (podium) modular, a separate structural frame — often a concrete or steel frame, or a podium structure — carries the loads, and the modules are either supported by that frame floor by floor or infilled within it, rather than carrying the building themselves. This decouples the modules from the primary structure and brings real freedom: you can open up the ground floor for shops, parking, a lobby or a double-height space (the module stack does not need to run all the way to the ground), you can build taller because the frame, not the modules, resists the big loads, and you can mix modular accommodation above with conventional space below. The cost is a second structural system to build and coordinate, and the interface between frame and module to detail.
Many real buildings combine the two: a conventional in-situ or steel podium at the base (providing the active, varied ground floor and transferring loads), with load-bearing modules stacked above. The choice between load-bearing and frame-supported — and where to transition — is an architectural and structural decision that must be taken early, because it governs height, the ground floor, the module design and the whole logic of the building. As always, the binding structural design of either system, and of the transfer between them, belongs to the qualified structural engineer and the manufacturer's tested system under NBC India; the designer owns the strategic choice and its architectural consequences.
Load-bearing: modules carry modules (regular stack, height-limited). Frame-supported/podium: a frame carries the load (open ground floor, taller, mixed). Decide early.
Designing volumetric well: freeze early, repeat, detail the joint, be honest
Volumetric rewards a particular way of working, and fighting it is how modular projects go wrong. Four disciplines matter most.
First, decide and freeze early. Because the factory needs the module design frozen to begin, the off-site decision and the key module dimensions, layouts and services must be settled at concept and scheme, when a site-built project would still be fluid. A client who wants to keep options open, or a design that will evolve through construction, is a poor fit for volumetric. The discipline is front-loading: do the hard thinking early, then hold it.
Second, design for repetition. Volumetric's economics live on building the same module many times, so the design should concentrate on a small number of well-resolved module types repeated often, rather than many bespoke ones. Variety should come from how modules are arranged, stacked, stepped, clad and combined with site-built elements — the facade, the roof, the ground floor — not from making every module different. This is the kit-of-parts thinking the next lesson develops: a disciplined, repeated module yielding architectural variety through arrangement.
Third, detail the interfaces and the joint. The module-to-module double skin, the module-to-podium connection, the module-to-facade junction and the on-site services connections are where a stack of boxes becomes a building, and they carry the structural, fire, acoustic and weather performance across lines of discontinuity. A volumetric building's quality lives in these joints, and they must be designed to go together quickly, accommodate real tolerance, and perform — not be improvised on site, which a finished module does not allow.
Fourth, be honest about fit. Volumetric is spectacular where repetition, a suitable site (accessible for big lorries and cranes), a frozen brief and a reasonable transport distance all line up — and a poor, expensive choice where the building is varied, the brief will change, the site is tight or distant, or the volumes are low. In India, the transport and craneage cost of shipping finished boxes, and the prevalence of varied, evolving briefs, mean volumetric suits specific high-repetition, high-speed applications (hotels, institutional accommodation, healthcare, and especially bathroom pods) rather than being a default. The binding structural, fire, acoustic, transport and lifting engineering, and the honest business case, belong to the structural, fire and acoustic engineers, the manufacturer's tested and warranted system, the transport and lifting specialists, the quantity surveyor and NBC India. The designer owns the go/no-go judgement, the module and building design, the repetition strategy and the interfaces — and the honesty to recommend against volumetric when the project does not fit it.
Transport envelope & craneage
Maximum module size, weight and the lift
Road width/height/length limits, permits, the route and crane capacity set the maximum module — hard constraints fixed by transport and lifting specialists and local rules, not by the designer's preference. Figures here are illustrative.
Load-bearing vs frame-supported
How the building carries its loads
Load-bearing stacks modules directly (regular, height-limited); frame-supported/podium uses a separate frame (open ground floor, taller, mixed use). The strategic choice is the designer's; the binding structural design is the engineer's and the manufacturer's under NBC India.
Double-skin joint (module-to-module)
Structure, fire, acoustics and weather across module junctions
The back-to-back walls and floors where modules meet must be designed for compartmentation, acoustic separation, load transfer and weather — by the fire, acoustic and structural engineers and the manufacturer's tested system.
Design freeze & the business case
When decisions must be fixed, and whether volumetric pays
The factory needs the module design frozen early; the cost-and-time case depends on repetition, site and logistics. The QS and team establish whether it actually stands — never assumed. Modules 7 and 9.
Workshop — test a building for volumetric, and size a module
Volumetric is a powerful tool with a narrow fit. In this workshop you will test a real building type against that fit, size a module to a transport envelope, choose a structural strategy, and decide honestly whether volumetric is the right answer.
A repetitive building type and a notebook. No real transport or structural calculation — the envelope and strategy here are illustrative reasoning; the binding limits come from the transport, lifting and structural specialists.
Goal: judge volumetric fit and size a module
Inputs: a building type with repeated rooms (hotel, student block, ward, apartments) + this lesson + a notebook
Time: ~50 minutes
- 1Score the fit: rate your building type against volumetric's five rewards/punishments — repetition (many identical rooms?), brief stability (will it change?), site access (can big lorries and a crane reach it?), transport distance (how far from a factory?), and programme pressure (is speed valuable?). Write an honest overall verdict: good fit, poor fit, or partial.
- 2Size a module: take the most-repeated room and sketch it as a box. Assume an illustrative road transport envelope (a maximum width, height and length — flag these as figures to confirm with a transport specialist, not a specification) and check whether your room fits within it, or must be split into two modules.
- 3Choose a structural strategy: decide whether this building should be load-bearing modular (regular stack) or frame-supported/podium (open ground floor, taller, mixed use), and justify the choice against the ground-floor use and height.
- 4Detail the double skin: sketch the junction where two of your modules meet (side-by-side or stacked), showing the two back-to-back walls/floors and noting what the joint must do for structure, fire, acoustics and weather.
- 5Write a one-paragraph verdict: whether volumetric fits this building, the module size and structural strategy you chose, and what the double-skin joint must achieve — with the binding transport, craneage, structural, fire and acoustic engineering, and the cost case, explicitly handed to the specialists, the manufacturer, the QS and NBC India.
You’ll walk away with
A one-page volumetric test: an honest fit verdict, a module sized to an (illustrative) transport envelope, a chosen structural strategy and a double-skin joint sketch. Keep it; the next lesson shows how to combine volumetric with panels and pods when full volumetric does not fit.
Three altitudes on the same idea
Read the band that fits you — or all three.
Volumetric is the biggest off-site commitment you can lead, and its design logic is unforgiving: decide early, freeze early, repeat. Your decisions are the go/no-go call (does this project's repetition, site access, transport distance and brief stability actually suit volumetric?), the module dimensions set by the transport envelope and craneage, the structural strategy (load-bearing for regular repetitive stacks, frame-supported/podium for open ground floors, height and mixed use), the repetition strategy (few well-resolved module types, variety from arrangement, facade, roof and ground floor), and the interfaces — the module-to-module double skin, module-to-podium and module-to-facade joints where the building's performance lives. Front-load the hard thinking and hold it; volumetric punishes late change. Defer the binding structural, fire, acoustic, transport and lifting engineering and the cost case to the specialists, the manufacturer's tested system, the lifting engineers, the QS and NBC India — and have the honesty to say no when the project does not fit.
Volumetric is where interiors get made in the factory — a module often arrives with finishes, joinery, bathroom and kitchen fittings and even furniture installed, so interior decisions are locked far earlier than on any site-built job. Your work moves forward in the programme: you must resolve layouts, finishes, fittings and service positions to the factory's freeze date, coordinate them with the module's structure and the double-skin walls, and design the repeated room to be exactly right, because it will be built hundreds of times. Watch the interfaces — where modules meet, where the module meets the corridor or facade, where finishes must resolve across a joint — and coordinate any fire-rated or acoustic element with the manufacturer and engineer rather than assuming the module carries it. Repetition is your ally: getting one room perfect pays off at scale.
Volumetric modular is the dramatic far end of the spectrum — whole finished rooms built in the factory and stacked on site — and understanding its costs as clearly as its promise is what separates a hype view from a competent one. Learn the promise (maximum factory value, maximum speed from parallel factory-and-site work, quality from repetition) and the five costs (weight, transport envelope, handling fragility, dimensions locked in early, the double skin at module joints), and the two structural strategies (load-bearing versus frame-supported/podium). Above all, internalise that volumetric rewards repetition, early certainty and suitable logistics and punishes variety, late change and difficult sites. You are not asked to engineer a module or its lift; you are asked to understand the system, design to its discipline, and judge honestly where it fits — which for volumetric means knowing when to recommend against it.
“Volumetric modular is the most advanced form of off-site construction, so it is the best choice whenever you can afford it — the goal every serious prefab project should aim for.”
Do it yourself
No tools needed — reason it through.
- 1Describe what a volumetric module is and the specific situation in which it shines — and why repetition is the key.
- 2Explain the two sources of volumetric's dramatic speed, including why parallel factory-and-site working matters most.
- 3Name the five costs of maximum factory value, and why 'dimensions locked in early' is the deepest for a designer.
- 4Contrast load-bearing and frame-supported (podium) modular, and say what each enables and limits.
- 5Why is 'volumetric is the most advanced, so aim for it whenever you can' a mistaken view?
The one line to carry out
Peer-reviewed journals & authoritative standards
- 01Modular building — Wikipedia — Modular building, 2026.
- 02Volumetric (construction) — Wikipedia — Volumetric (construction), 2026.
- 03Intermodal container — Wikipedia — Intermodal container, 2026.
- 04Nakagin Capsule Tower — Wikipedia — Nakagin Capsule Tower, 2026.
- 05Oversize load — Wikipedia — Oversize load, 2026.
Full volumetric rarely suits a whole building — but its best trick, the finished room, can be dropped into buildings that are otherwise panelised or site-built, and the spectrum can be mixed pragmatically. Next: pods, hybrids and the kit-of-parts.
The author
Amogh N P
Architect, interior designer, and creative polymath. Studio Matrx began in his notebooks — his vision of design made honest, useful, and open to everyone. Its Academy is written and taught in his memory, and free, forever.
More about Amogh →