
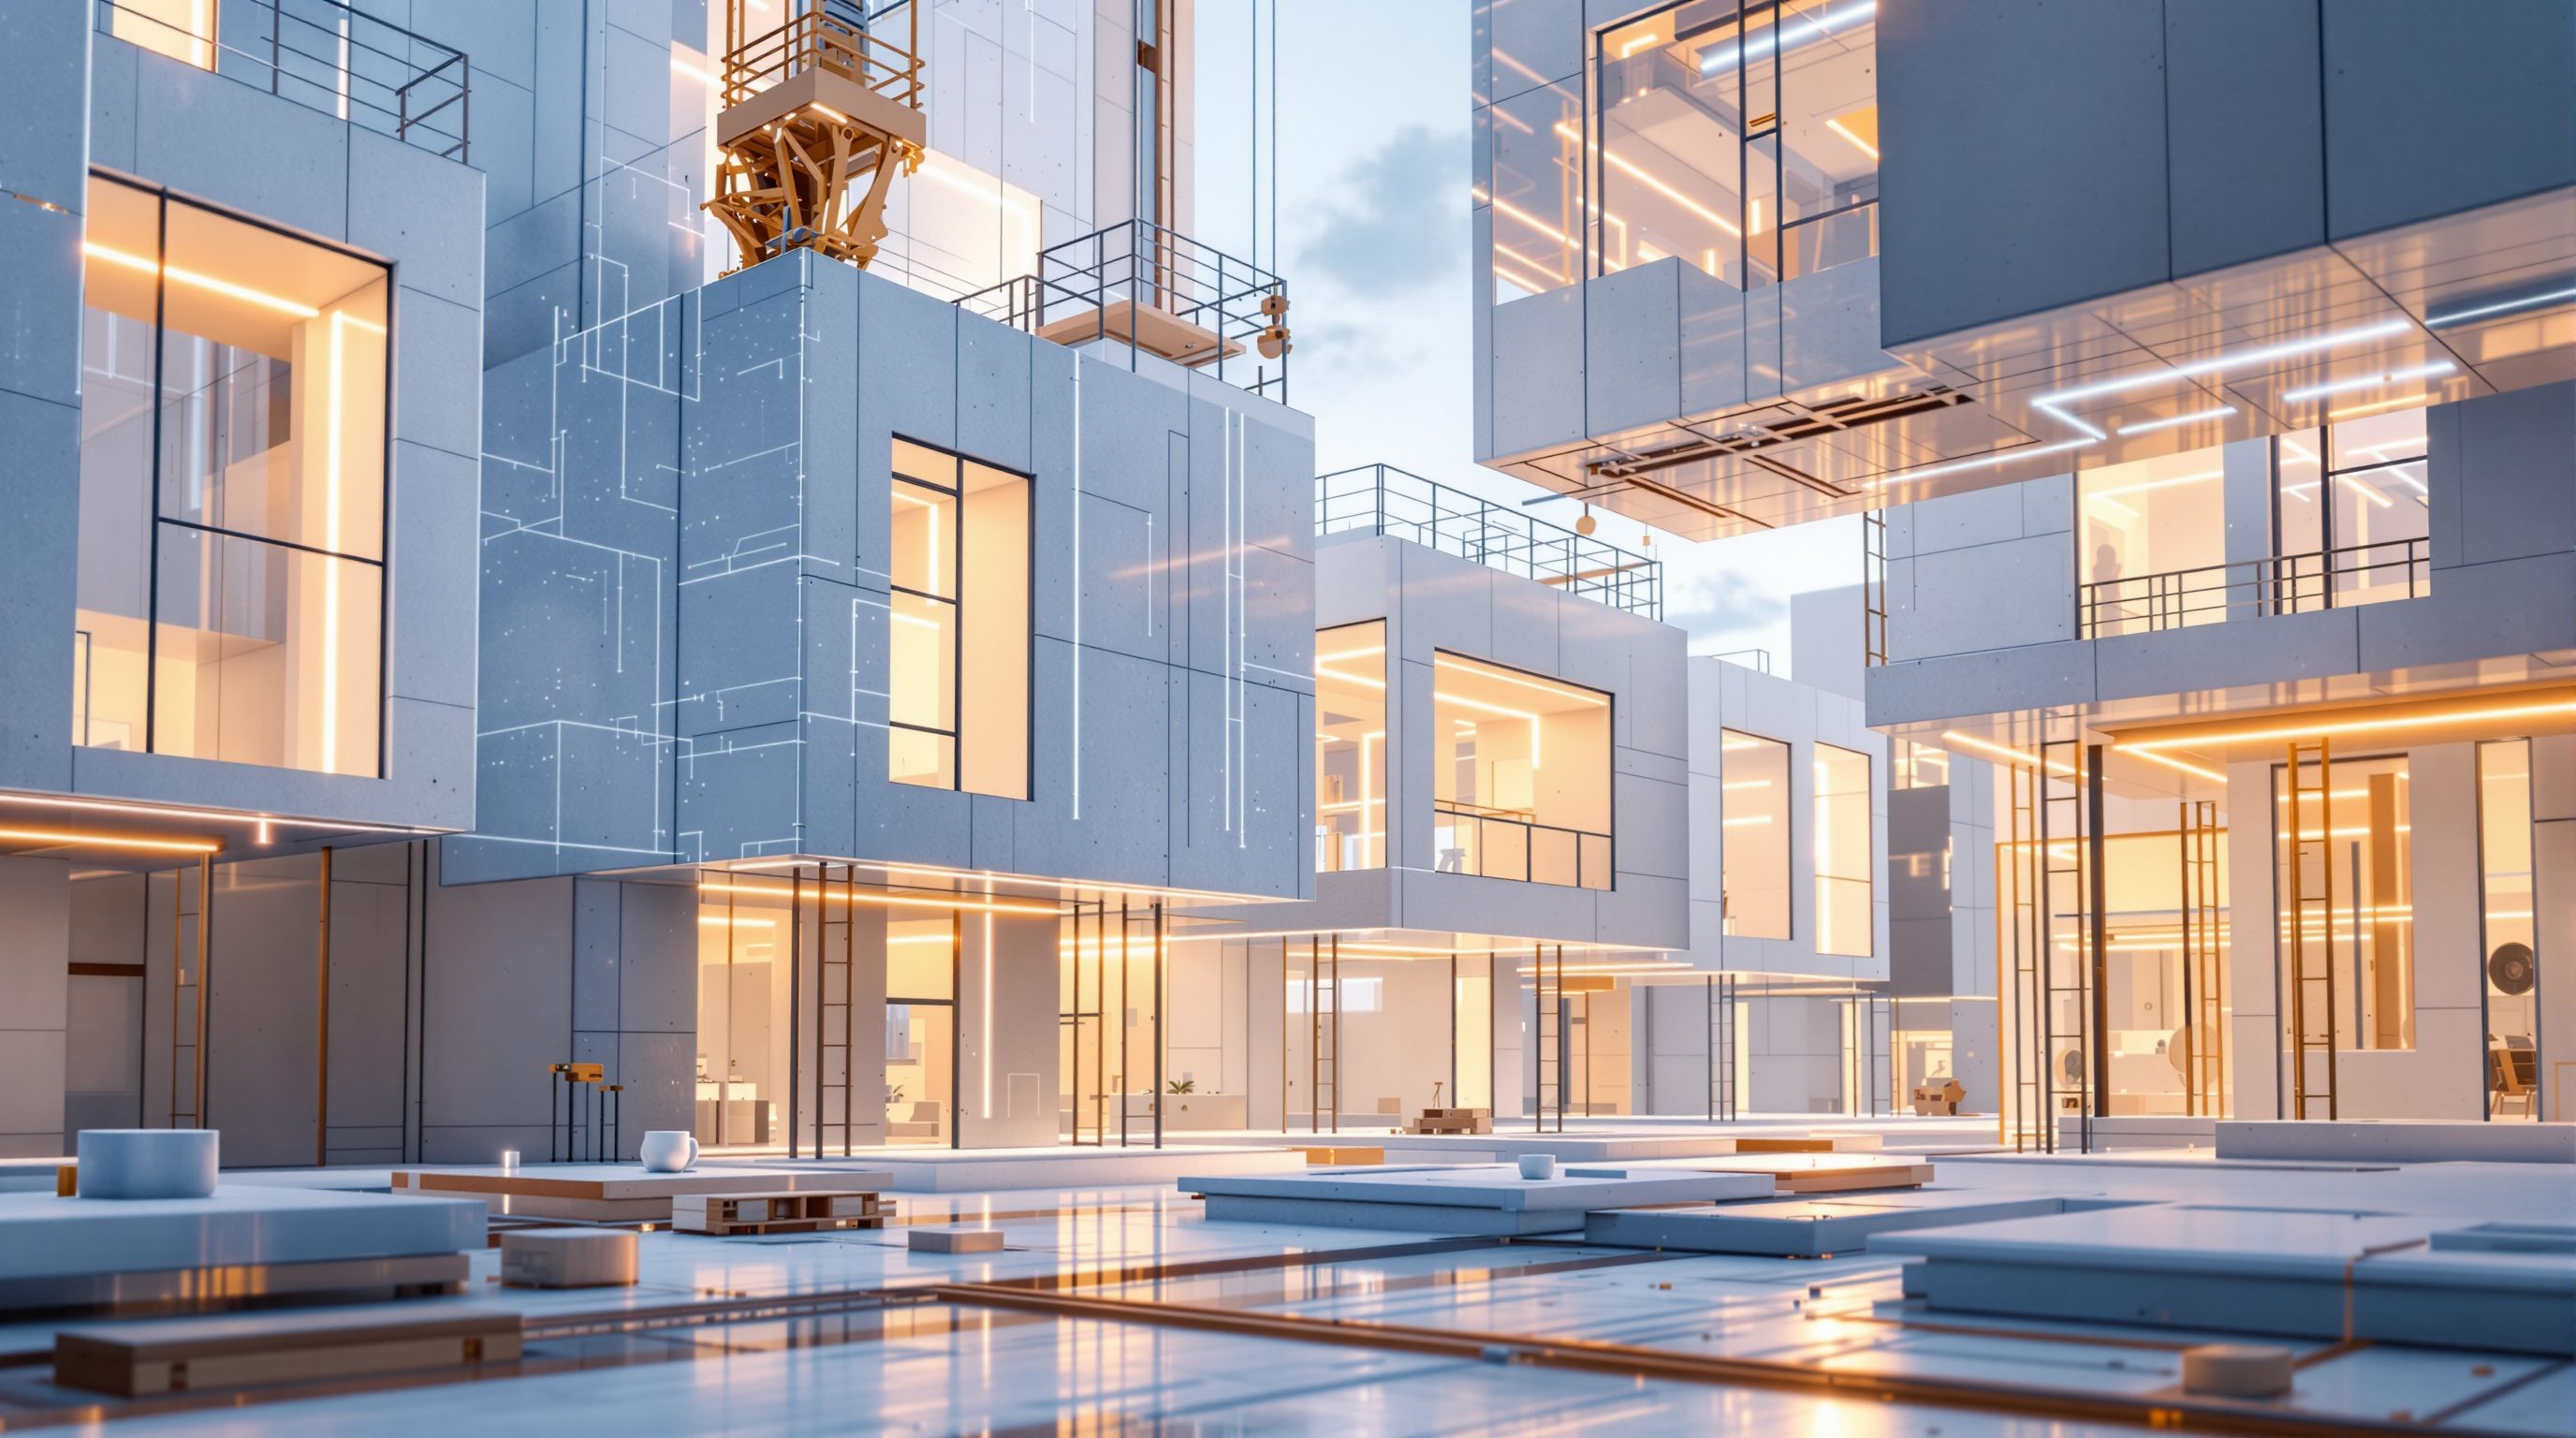
 Lesson 4.3
 · Materials & Structural Systems
Precast & Modular Concrete
Cast in a clean factory bed instead of a muddy site, concrete becomes a precise, massively durable, fire- and sound-resistant off-site product -- heavy, certainly, but the material in which India's prefab capability already runs deepest
Take the one building material India already makes at vast scale, cast it in a clean factory bed under quality control instead of in a muddy formwork on site, and you get precise, massive, fireproof, hundred-year components -- if you can lift and move them.
Concrete is the material of modern India -- poured into billions of square metres of frame, slab and wall every year. Almost all of it is cast in situ: wet concrete tipped into formwork on site, propped, and left to cure in the heat and dust before the next floor can rise. Precast concrete moves that casting off the site and into a factory. Instead of building formwork in the air, you cast the element flat or in a mould in a controlled yard -- a wall, a floor plank, a beam, a staircase, or a whole room-sized box -- cure it under ideal conditions, and deliver the finished, hardened component to site to be lifted into place.
That single move gives concrete the factory virtues this module keeps returning to: controlled conditions, repeatable quality, parallel working while the foundations go in, precise dimensions and a fine cast finish -- plus everything concrete is already famous for: mass, robustness, fire resistance, acoustic performance and extraordinary durability. It is the heaviest of the three material families, and that weight is the root of its challenges -- transport, craneage, and a significant embodied-carbon burden. But precast is also the material in which India's off-site capability runs deepest: the country has a mature precast industry serving large, repetitive housing, infrastructure and institutional projects. This lesson teaches how precast works, what it is genuinely good at, what it costs, and how to design with it -- deferring, as ever, the structural, connection and fire design to your engineers, the manufacturer's system and the code.
Precast: the factory-cast heavyweight. Mass = great sound + fire + durability. Weight = big cranes, hard transport, high carbon. Joints don't exist till you make them.
The precast family: panels, planks and volumetric cells
Precast is not one product but a family, spanning the same spectrum from flat component to whole room that you met in Module 2 -- and knowing the members of that family is the start of designing with it. At the 2D end are panels: flat slabs of concrete cast in the factory and stood up on site as walls (structural loadbearing walls, or non-loadbearing cladding and facade panels, including richly finished "architectural" precast) and as floor and roof elements. A hugely important floor product is the hollow-core plank -- a precast floor unit with continuous tubular voids running through it, which remove weight and concrete from where the element does little work, giving a lighter, longer-spanning, material-efficient floor that is craned into place and needs little or no propping. Alongside these sit precast beams, columns, stairs and landings -- the staircase in particular is a classic precast win, delivered as a finished flight rather than built laboriously in situ.
At the 3D end are volumetric precast modules -- whole room-sized "cells" or boxes cast in concrete, complete with walls, floor and ceiling, and increasingly with services and finishes, craned into place and stacked. A familiar example is the concrete bathroom or service pod; at larger scale, entire cellular rooms -- prison cells, hotel rooms, apartment modules -- are cast as concrete boxes. Because concrete is so heavy, volumetric precast pushes transport and craneage hard, so it is used where its mass, durability, fire and acoustic performance are worth the lifting.
In between sits a spectrum of hybrid and composite approaches that are very common and very sensible: precast elements combined with in-situ concrete to marry factory quality with on-site continuity. Examples include half-slab or "filigree" floors (a thin precast soffit plank that acts as permanent formwork and is topped with in-situ concrete to make a composite slab) and precast twin-wall panels (two precast skins connected by lattice girders, stood up and filled with in-situ concrete). These hybrids capture much of precast's quality -- a perfect soffit, no temporary formwork, parallel working -- while keeping the monolithic continuity and simpler connections of in-situ concrete. Choosing where on this family tree a project sits -- panel, plank, hybrid or full volumetric -- is a central precast design decision.
Precast spectrum: flat panel -> hollow-core plank -> beams/stairs -> half-slab & twin-wall hybrids -> whole volumetric cell. Heaviest family, deepest Indian capability.
Why cast off-site: quality, mass, fire, durability
The case for precast rests first on the same factory logic as the rest of the module, and then on a set of performance gifts that are uniquely concrete's. The factory logic: casting in a controlled yard, in reusable steel or timber moulds, under proper curing, produces concrete of higher and more consistent quality than pouring into site formwork exposed to heat, rain and variable workmanship -- denser, better compacted, more accurately dimensioned, with a superior cast finish that can be left exposed as the final surface. The moulds are used over and over, so repetition pays; the work proceeds in parallel with site groundwork; waste is controlled; and much of the dangerous, slow in-situ work at height is removed.
On top of that sit concrete's intrinsic performances, which are precisely the ones lightweight steel and timber must work hard to achieve. Mass: a concrete element is heavy and dense, and mass is exactly what blocks airborne sound, so precast walls and floors give excellent acoustic separation almost inherently -- a major reason precast suits apartments, hotels and party-wall-heavy buildings. Fire: concrete is non-combustible and a poor conductor of heat, so it has excellent inherent fire resistance, protecting its reinforcement and maintaining structure for long periods -- often with little or no added fire protection. Robustness and durability: a well-made concrete element is hard, impact-resistant, and extraordinarily long-lived, shrugging off weather, wear and time in a way timber and thin steel cannot, which is why concrete dominates infrastructure and long-design-life buildings.
Add thermal mass (concrete's ability to absorb, store and release heat, which can be used to moderate indoor temperature swings -- relevant in many Indian climates), and good water and pest resistance, and you have a material that delivers heavy-duty performance with minimal fuss once it is in place. The trade, of course, is that all of this comes *with the weight* -- and the weight is the source of every one of precast's challenges, which the next section takes head-on. But where mass, fire, acoustics and a hundred-year life are what the building needs, precast is the material that supplies them as a matter of course.
The honest challenges: weight, transport, craneage, carbon, connections
Precast's challenges follow, almost without exception, from its defining virtue -- mass -- and from the fact that the elements are finished, hardened and rigid before they ever reach the site. The first and most obvious is weight. A precast panel or, especially, a volumetric concrete cell is enormously heavy compared with a steel or timber equivalent, and that weight drives everything downstream: it demands large, expensive cranes with the capacity and reach to lift it (craneage can be a defining cost and logistical constraint), it limits how far and how easily elements can be transported (heavy loads, escort and permit requirements, road and bridge limits -- all firmly the domain of transport specialists and local rules), and it pushes foundation sizes up, since the ground must carry a heavier superstructure. Where steel and timber shrink the crane and the footing, concrete enlarges them.
The second challenge is embodied carbon. Cement, concrete's binder, is responsible for a large share of global carbon emissions, so concrete -- precast included -- carries a significant embodied-carbon burden, the mirror image of timber's low-carbon story. Precast can mitigate this (efficient sections like hollow-core that use less material, cement replacements, longer service life spreading the impact), but it remains a serious honest mark against the material in a decarbonising world, and one you should weigh openly.
The third, and most design-critical, is connections. A precast building is an assembly of discrete hard elements that must be joined to act as one structure and to perform for fire, weather and sound -- and unlike monolithic in-situ concrete, those joints do not exist until you make them. Precast connections -- bolted or welded plates, projecting reinforcement loops lapped and grouted, in-situ concrete stitches, bearing details -- are the crux of the system: they must transfer load, accommodate tolerance, resist fire and water, and be safely made at height, and their design is demanding structural engineering that belongs wholly to your engineer and the manufacturer's tested system. Add the practical points -- elements are rigid and cannot be trimmed or adjusted on site (so dimensional accuracy and setting-out must be right first time), and they are vulnerable to handling and transport damage at their edges and corners -- and the message is clear: precast rewards early certainty, accurate coordination and rigorous connection design, and punishes improvisation.
Every precast problem traces back to weight: big cranes, hard transport, bigger foundations, high carbon. Plus: the joints don't exist till you make them -- engineer them.
Designing with precast -- and its strong fit in India
Designing in precast is, above all, an exercise in designing for the joint, the mould and the lift. Because elements are finished before they arrive and cannot be altered on site, the dimensional discipline is absolute: you work to a grid, standardise elements so a few moulds are reused many times (repetition is where precast's economics live), and resolve every connection and interface in the model before anything is cast. You design the lifting and handling -- where the crane hooks on, how the element is the right way up, how it is temporarily propped until the connections are made -- as part of the design, not an afterthought. And you design the finish deliberately, since a precast surface can be the final architectural face (exposed aggregate, textured, coloured, formliner-patterned) and that decision shapes the mould.
It is worth stressing where precast *fits*, because it is sharply different from light steel and timber. Precast rewards large, repetitive projects -- many identical apartments, hotel rooms, school classrooms, stadium terraces, infrastructure elements (bridge beams, metro segments, tunnel linings, boundary walls) -- where the mould is reused endlessly and the weight is justified by the performance. It is less suited to small, one-off or highly bespoke buildings where the mould cost cannot be amortised and the craneage cannot be justified. The mass, fire and acoustic performance make it a natural for party-wall-heavy residential, and its durability for long-life and hard-wear buildings.
And here the Indian context flips the usual script. Where timber is niche and light-gauge steel is still growing in India, precast concrete is the material in which Indian off-site capability runs deepest and most proven: India has a substantial, maturing precast industry -- dedicated plants and experienced players serving large affordable-housing missions, townships, commercial, institutional and infrastructure programmes -- and the economics suit the country's vast, repetitive construction pipeline. The familiar material, the established supply chain, the performance in a hot climate (thermal mass, durability, pest and fire resistance) and the fit with scale all make precast the most immediately realistic large-scale off-site system in India today. Its real constraints here are the same as everywhere -- craneage and transport logistics, the embodied-carbon question, and the absolute need for correct connection design -- all of which remain with the engineers, the manufacturer's system, the transport specialists and the code.
Precast concrete elements
Element types, reinforcement, spans and finishes
Section design, reinforcement, spans and mix are structural outputs tuned to the loads and the mould -- the descriptions here are principle, not specification.
Connections & grouting
How discrete elements are joined to act as one
The crux of precast: connection design (grouted loops, plates, in-situ stitches, bearings) is demanding structural engineering for the engineer and the tested system. Module 5.3.
Craneage & transport limits
Lifting heavy elements and moving them to site
Crane capacity/reach and heavy-load transport permits and routes are hard constraints set by lifting and transport specialists and local rules. Module 7. Figures are illustrative.
Embodied carbon & NBC India
Carbon burden of cement; regulatory approval
Concrete carries a significant embodied-carbon burden to weigh openly; and the National Building Code of India and local rules govern approval via the manufacturer and design team.
Workshop -- match a precast strategy to a repetitive building
Precast shows its logic on large, repetitive buildings, where you trade mould cost and weight for quality, performance and speed. In this workshop you will take one repetitive building type and reason through which precast family members fit, what the weight demands, and where the connections and carbon questions sit -- seeing precast as a kit of hard parts you assemble.
A repetitive building type, this lesson's figures, paper and a pen. No calculation -- this is strategy and judgement, not structural design.
Goal: a qualitative precast strategy for one repetitive building
Inputs: a large repetitive building type (an apartment block, a hostel, a school, a metro station) + this lesson + a notebook
Time: ~45 minutes
- 1Pick the building and count the repetition: choose a repetitive building type and identify the most-repeated elements -- the same wall, floor bay, room or stair occurring many times. That repetition is precast's economic engine.
- 2Choose family members: decide which precast products fit -- loadbearing or cladding panels, hollow-core planks for the floors, precast stairs, a half-slab or twin-wall hybrid, or whole volumetric pods -- and say why each suits this building.
- 3Follow the weight: for your heaviest element, reason through what the weight demands -- crane capacity and reach, transport and access to site, foundation implications -- and flag craneage and transport as questions for the specialists.
- 4Map the connections: pick one junction (panel-to-panel, plank-to-wall, module-to-module) and describe, in principle, how it would be joined and what it must do (carry load, resist fire and water, take tolerance) -- flagging the design for the engineer.
- 5Weigh carbon and write the verdict: note the embodied-carbon burden and one way to reduce it (efficient sections, cement replacement, long life), then give a one-paragraph honest call on precast's fit for this building -- as reasoning, not a specification.
You’ll walk away with
A one-page precast strategy: the repetition identified, the family members chosen, the weight consequences, one connection reasoned in principle, the carbon weighed, and an honest fit verdict -- showing you can treat precast as an assembled kit of hard parts.
Three altitudes on the same idea
Read the band that fits you — or all three.
Precast is a decision about mass, repetition and logistics taken at concept. It rewards large, repetitive projects -- many identical apartments, rooms, classrooms, or infrastructure elements -- where a few moulds are reused endlessly and concrete's inherent fire, acoustic and durability performance earns its weight; it is poor for small bespoke one-offs. Set a standardising grid, decide where the project sits on the family tree (panel, hollow-core, half-slab/twin-wall hybrid, or full volumetric), and design the lifting, propping and finish as first-class moves. Treat the connections and interfaces as the heart of the design and resolve them early, because elements cannot be trimmed on site. Weigh the embodied-carbon burden openly against timber and steel. In India, lean on the country's deep, proven precast capability. Defer the structural and connection design, the craneage and transport limits, and the fire engineering to your engineers, the manufacturer's tested system, the transport specialists and the code.
Precast gives you a hard, massive, fire- and sound-resistant shell -- and a finish decision to make at casting. The great interior gift of precast is acoustic separation: concrete's mass inherently quietens party walls and floors, a real advantage in apartments and hotels -- respect and do not compromise the separating elements. The great discipline is that a precast surface can be the *finished* surface (a fair-faced, textured or coloured soffit and wall), which is decided in the mould long before you arrive, so coordinate early if you want exposed concrete as the interior character. You cannot chase services freely into structural precast, and fixings need cast-in sockets or inserts planned before casting -- so your setting-out for services, fixings and penetrations must feed the factory. In volumetric concrete pods and modules, exploit the robust, durable, true surfaces. Coordinate wet areas, service routes and fixings with the manufacturer so interior and element are one design.
Learn precast as the heavy, high-performance, most-Indian of the three families. Know the family -- panels, hollow-core planks, beams and stairs, half-slab and twin-wall hybrids, and whole volumetric cells -- and why casting in a factory gives better, more consistent quality and finish than site pours. Hold the strengths: mass (hence excellent acoustics), inherent fire resistance, robustness and a hundred-year durability, thermal mass. Hold the challenges, all rooted in weight: big cranes, hard transport, larger foundations, a significant embodied-carbon burden, and connections that must be engineered because the joints do not exist until you make them. Understand that precast rewards large repetitive projects and punishes bespoke one-offs, and that it is the most proven large-scale off-site system in India. You need not design a connection; you must grasp the system, design to its dimensional and lifting discipline, and know its fit. A commercially vital skill in the Indian market.
“Precast is just site concrete made somewhere else -- so it behaves exactly like a normal monolithic concrete building, the joints between panels are a trivial detail, and choosing it is simply about where you pour.”
Do it yourself
No tools needed -- reason it through.
- 1Name the main members of the precast family from flat panel to volumetric cell, and say what a hollow-core plank and a twin-wall or half-slab hybrid each do.
- 2Give three performance gifts concrete brings inherently (think mass, fire, durability) and why each matters for a building type.
- 3Explain how every major precast challenge traces back to weight.
- 4Why are connections the crux of a precast structure, and how does this differ from cast-in-situ concrete?
- 5Why is precast the most proven large-scale off-site system in India, and what are its real constraints here?
The one line to carry out
Peer-reviewed journals & authoritative standards
- 01Precast concrete — Wikipedia -- Precast concrete, 2026.
- 02Structural engineering — Wikipedia -- Structural engineering, 2026.
- 03Crane (machine) — Wikipedia -- Crane (machine), 2026.
- 04Embodied carbon — Wikipedia -- Embodied carbon, 2026.
- 05National Building Code of India — Wikipedia -- National Building Code of India, 2026.
Now you have met all three material families -- light-gauge steel, timber and mass timber, and precast concrete -- each with a distinct grain of strengths and costs. The final lesson of the module puts them side by side and builds an honest framework for choosing between them (and their hybrids) for a given building.
The author
Amogh N P
Architect, interior designer, and creative polymath. Studio Matrx began in his notebooks — his vision of design made honest, useful, and open to everyone. Its Academy is written and taught in his memory, and free, forever.
More about Amogh →